Why Laser Engraving Depth Control Matters in Industrial Applications
In high-stakes manufacturing environments—from aerospace to medical device production—laser engraving depth control settings are not optional; they are mission-critical. Precise depth ensures regulatory compliance, long-term part traceability, and functional integrity. Over-engraving can compromise structural strength; under-engraving risks legibility failure during field inspections or recalls. At MeykoLaser, our industrial laser marking machines integrate advanced depth control algorithms to deliver repeatable, ISO-compliant engraving across diverse materials.
How Laser Engraving Depth Is Controlled: The Technical Foundation
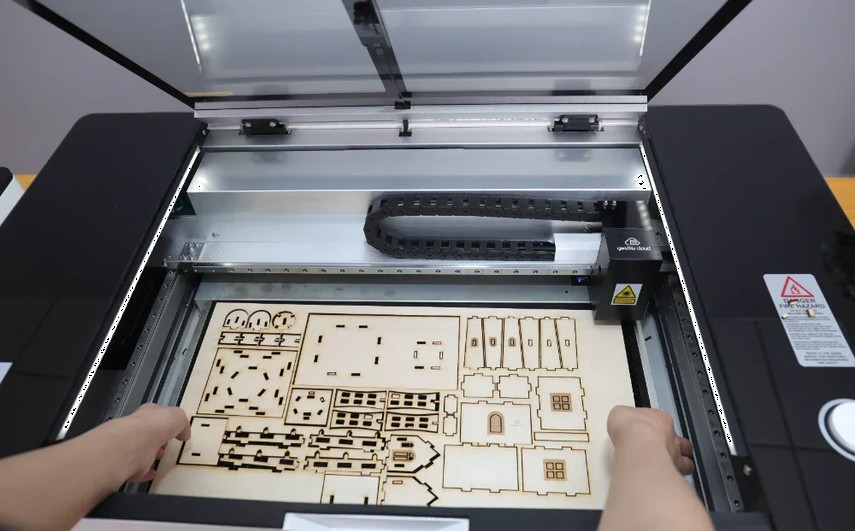
Depth control in laser marking is governed by three interdependent parameters: laser power, pulse frequency, and scanning speed. Unlike surface marking, depth engraving requires energy accumulation over multiple passes or optimized single-pass ablation. Our machines use closed-loop Z-axis control to dynamically adjust focal height, ensuring consistent energy density regardless of material warpage or surface irregularities.
Key Parameters Affecting Engraving Depth
- Laser Power (W): Higher power increases material ablation rate, but excessive power causes thermal damage and recast layers. MeykoLaser’s fiber lasers offer 20–100 W adjustable output with ±0.5% stability.
- Pulse Frequency (kHz): Lower frequencies (e.g., 20–50 kHz) deliver higher peak power per pulse, ideal for deeper engraving on metals. Higher frequencies (100–200 kHz) produce finer, shallower marks.
- Scan Speed (mm/s): Slower speeds increase dwell time, deepening engraving. Our machines support speeds from 10–10,000 mm/s with 0.1 mm/s resolution for fine-tuned control.
Material-Specific Depth Optimization
Depth behavior varies significantly by material. MeykoLaser’s built-in material database includes pre-validated settings for common industrial alloys, plastics, and ceramics:
- Stainless Steel (304/316)
- Aluminum Alloys: Prone to oxide layer formation. Using 30–40 kHz with 40 W and a 150 mm/s pass achieves 0.15 mm without excessive surface roughness.
- Engineering Plastics (PC, PEEK): Require lower power (15–25 W) and higher frequency (80–120 kHz) to prevent melting; depths of 0.08–0.15 mm ensure durability without compromising tensile strength.
Advanced Depth Control Features in MeykoLaser Machines
Our latest MK-DeepEngrave Series integrates proprietary technologies that eliminate guesswork in depth tuning:
- Real-Time Depth Monitoring: Integrated confocal displacement sensors measure engraving depth during operation, auto-adjusting parameters to maintain ±0.01 mm tolerance.
- Adaptive Pulse Shaping: Customizable pulse waveforms (square, trapezoidal, ramp) optimize heat diffusion for materials like titanium where brittle fracture must be minimized.
- Multi-Pass Depth Stacking: Software-controlled pass sequencing (e.g., 3-pass zigzag → 2-pass fill) enables depths up to 0.8 mm on hardened tool steels without thermal distortion.
Quantifiable Business Benefits of Precise Depth Control
Investing in machines with superior laser engraving depth control settings delivers measurable ROI:
- Reduced Scrap Rates: Precision depth control minimizes over-removal on high-value components. One medical device OEM reported a 22% drop in rework after switching to MeykoLaser.
- Compliance Assurance: Engraved UDI codes meet FDA 21 CFR Part 820 and EU MDR depth and contrast requirements—verified by third-party image analysis tools included in our software.
- Extended Tool Life: By avoiding unnecessary high-power operation, our fiber laser sources last 100,000+ hours (vs. industry avg. 80,000).
Implementation Guide for Procurement Managers
When evaluating laser marking systems, prioritize depth repeatability over peak power. Request a depth validation report for your specific material. MeykoLaser provides:
- 3-axis profilometry scans of test samples (Ra, Rz, depth profiles)
- Statistical process control (SPC) charts for 100-part runs
- Material-specific depth calibration certificates (ISO/IEC 17025 accredited)
Don’t settle for generic specs—demand performance data for your application.
Frequently Asked Questions (FAQ)
How does MeykoLaser ensure consistent engraving depth across different industrial materials?
MeykoLaser uses closed-loop Z-axis control to dynamically adjust focal height and balance energy density across varied materials. This is achieved through tightly controlled laser power, pulse frequency, and scanning speed. The machine integrates a material database with pre-validated settings, allowing repeatable, ISO-compliant engraving depth without thermal damage or uneven surfaces.
What are the recommended settings for achieving 0.15 mm depth engraving on stainless steel or aluminum alloys?
For stainless steel 304/316 and aluminum alloys, MeykoLaser recommends 30–40 kHz pulse frequency, 40 W laser power, and 150 mm/s pass speed. These parameters provide 0.15 mm depth while reducing surface roughness. The pre-validated database ensures consistent performance and minimizes oxide layer effects.
How does scanning speed affect laser engraving depth, and how does MeykoLaser manage it?
Lower scanning speeds increase dwell time, which deepens engraving, while higher speeds produce finer, shallower marks. MeykoLaser supports speeds from 10 to 10,000 mm/s with 0.1 mm/s resolution, allowing precise adjustment to maintain required depth on complex parts without sacrificing performance.
How does MeykoLaser optimize engraving depth for engineering plastics such as PC or PEEK?
For engineering plastics like PC and PEEK, MeykoLaser uses lower power settings of 15–25 W combined with higher pulse frequencies of 80–120 kHz. This prevents melting and produces durable depths of 0.08–0.15 mm without compromising tensile strength on high-performance materials.
What technology does the MeykoLaser MK-DeepEngrave Series use to stabilize engraving depth on large parts?
The MK-DeepEngrave Series applies proprietary depth control technologies and closed-loop Z-axis adjustment. This system dynamically maintains focal height and energy density during processing, ensuring consistent engraving depth even when parts experience warpage or surface irregularities, improving repeatability and part integrity.